If you’re in the business of heavy-duty metal fabrication, construction, or any field that relies on precision drilling through thick steel, you know a magnetic drill press is far more than just another tool—it’s the backbone of your workflow. As a supplier of these machines, I’ve spent thousands of hours walking side by side with workshop managers, drill operators, and maintenance teams, watching them push their magnetic drill presses to the limit: boring 2-inch holes through 6-inch structural steel beams, drilling repetitive patterns for ship hulls, and powering through rusted plate that would stop lesser tools cold. Over time, one question rises to the top every single time: “How do I know my drill’s magnetic force is actually strong enough to get the job done safely?” Magnetic Drill Press
This isn’t just a theoretical concern. I’ve seen a shop foreman lose a $12,000 drill bit mid-cut because his drill’s magnetic base failed under the torque of a deep cut on a thick steel column. I’ve heard horror stories of operators nicked by a flying drill that slid sideways mid-operation, narrowly missing more severe injury. The worst part? Most of these issues aren’t a flaw in the machine itself—they’re a lack of consistent, practical testing for magnetic force. Too many operators rely on a quick visual check or the “feel” of the base sticking to steel, and that’s a mistake. Magnetic force isn’t just about holding the drill in place; it’s a core safety and performance metric that dictates how deep you can drill, what diameter bits you can use, and even how stable your cuts will be.
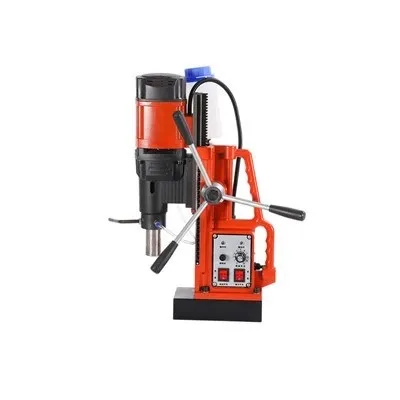
Let’s break this down into steps that actually work, using real-world methods I’ve observed and validated with every machine we sell. First, we need to understand what magnetic force in a drill press actually is. The base of the machine houses powerful rare-earth magnets, usually neodymium or ferrite-core electromagnets (most commercial models use electromagnets these days for adjustable force and on/off control). That force is measured in amps for powered models, or pull-force for permanent magnets, and it has to overcome two key forces during operation: the rotational torque of the drill bit and the downward force of the feed mechanism. If the magnetic force is lower than the sum of those two forces, the drill slips. Simple, right? But testing it accurately isn’t as simple as picking up a scale and pressing it to the base.
Before we jump into hands-on tests, there are a few pre-test checks to rule out avoidable errors that skew results. I can’t tell you how many times a test has gone wrong because the operator tested the drill on a piece of thin, corroded steel instead of a flat, clean test plate. Magnetic force is only measured against the contact surface of the material you’re drilling on, so surface conditions matter more than most people realize. A 1/16-inch thick layer of mill scale, rust, or paint can reduce effective magnetic force by 30% or more—enough to cause a slip on a deep cut. That’s a critical point: always test on the same grade of steel you’ll be using for jobs, at the same thickness, with a surface that’s been wire-brushed to a flat, uniform finish. For consistency, we recommend investing in a dedicated test plate: a 1-inch thick A36 steel plate, precision-machined flat on both sides, no rust or scale, with surface roughness of under 125 Ra. It’s a small investment that saves you from bad test results every time. Also, make sure the drill’s power source is consistent. If you’re testing a corded model, plug it into a dedicated 110V or 220V outlet (no extension cords longer than 10 feet, and no daisy-chaining) to avoid voltage drops that lower electromagnet output. For battery-powered models, use a fully charged, manufacturer-approved battery—old or replacement batteries can drop voltage by 15% or more mid-test, which is enough to skew readings.
Now, let’s get into the actual testing methods. I’ve sorted these from the most accessible (for small shops that don’t have fancy lab equipment) to the most precise (for industrial quality control). First, the static pull test. This is the go-to test for most operators because it requires no special tools beyond a few common items. Here’s how it works: first, attach your drill press to your prepared test plate, making sure the magnetic base is centered, pressed firmly to the steel, and there’s no gap between the base and the plate. For electromagnets, turn the power on and let it sit for 30 seconds to let the magnet fully engage (I’ve seen operators pull the trigger too fast, and the magnet hasn’t reached full output). Next, grab a high-quality digital scale (a kitchen scale won’t work—you need a scale that measures up to 1,000 pounds or more, with a precision of at least 5 pounds). Place the scale vertically, one side against the edge of the drill press’s frame (not the handle, not the cord mount), and the other side against a fixed, heavy object like a steel workbench leg. Then, use a long pipe or a pry bar to pull the drill press straight away from the test plate, parallel to the surface, in a slow, steady, upward motion. Don’t yank it—yanking will give you a false high reading. Keep pulling until the drill breaks free from the plate, and note the number on the scale. That’s your static pull force.
Wait, I know what you’re thinking: “That’s a great test, but does this translate to actual drilling force?” That’s the biggest gap in most operator testing, because static pull force is higher than dynamic force (the force the drill puts out while spinning). A static test might show a pull of 1,500 pounds, but when that force is spread over the rotational torque of a 2-inch drill bit moving through steel, the actual holding force can drop by 20-30%. That’s why we need a dynamic test, and for that, the easiest shop method is the torque test. This one requires a drill bit that’s compatible with your machine’s maximum bit diameter—let’s say a 2-inch annular cutter, the most common bit for heavy-duty drilling. Set up your test plate, attach the drill, and make sure all safety guards are in place. For this test, use a drill bit that’s designed for testing (so you don’t waste a valuable bit) and drill a shallow, ¼-inch deep hole at full power, using the same feed rate you would for a real job. Then, turn off the drill, leave the bit in the hole, and apply a lateral (side-to-side) force to the side of the drill’s head with a pry bar. If the drill doesn’t move at all, that means the magnetic force is enough to overcome the drill’s torque at that depth. If it shifts or slides, you have an issue. This test works because it mimics the actual lateral force the drill experiences when the bit is cutting through steel—way more accurate than a static pull.
For shops that do high-volume work or need precise, repeatable data, there’s a third test: the professional force gauge test. This one uses a digital force gauge, a tool that measures both axial and lateral force with high precision, usually accurate to within 1 pound. The process is similar to the static pull test, but instead of a scale, you mount the force gauge between the drill base and the test plate, or between the drill frame and a fixed anchor, to measure the exact force needed to break the magnet’s hold. Some industrial force gauges can even measure dynamic force while the drill is spinning, which is perfect for quality control checks on new machines. As a supplier, we use these force gauges for every drill press that leaves our warehouse—we don’t just rely on part numbers or specs, we test every unit to ensure it meets its rated magnetic force. That’s why when we send a new drill to a client, they can trust the specs they see on the label.
Now, let’s talk about common pitfalls that will throw all these tests off, because I’ve seen every single one of them. First, as I mentioned earlier, surface gaps. Even a tiny gap—less than 1/32 of an inch—between the magnetic base and the steel can reduce effective force by 50% or more. This can happen if the steel is warped, if the base has scratches or dents, or if you’re using a thin piece of test stock. Another pitfall is testing at extreme temperatures. If you’re testing outdoors in freezing weather, the magnet’s output drops significantly, while testing in temperatures over 100°F can also cause minor fluctuations. We recommend testing within a 50-80°F range for consistent results. Also, don’t forget about the magnet’s duty cycle. If you’re using your drill press for 8 hours straight, the electromagnet can heat up slightly, and while high-quality magnets are designed to handle that, lower-quality models may see a small drop in force after prolonged use. If you’re running long jobs, it’s a good idea to do a quick mid-shift test to make sure the force is still holding.
Now, why does all this matter for you as a user, and for us as your supplier? I mentioned earlier that I’ve seen operators get hurt because of a failed magnetic base. A drill press weighing 50-100 pounds, spinning a sharp steel bit, sliding across a work area is a serious hazard that’s completely preventable with proper testing. But it’s not just safety—performance too. If your magnetic force is lower than it should be, you’ll deal with slow cuts, excessive wear on your drill bits, and wasted time reworking holes that aren’t aligned. On the flip side, if you know your drill’s true magnetic force, you can push it to its safe limits: run larger bits, go deeper cuts, and keep your workflow moving without unnecessary pauses.

At the end of the day, the goal of testing magnetic force isn’t to overcomplicate your routine—it’s to make your job safer and more efficient. If you’re a shop manager looking to upgrade your fleet of magnetic drill presses, or an operator needing a reliable machine that can stand up to your toughest jobs, don’t just rely on the manufacturer’s specs. Ask for evidence of tested performance, and make sure you have a testing routine in place for every machine you bring into your shop. When you choose a supplier that stands behind the quality of their products, you get not just a tool, but the support to use it correctly. If you’re ready to learn more about how to test the magnetic force of your current drill press, or if you’re in the market for a new model that meets your specific force requirements, reach out to our team of experts to discuss your needs. We’re here to help you make the right choice for your work, every time.
Metal Lathe References
- American National Standards Institute (ANSI B10.60-2018) Safety Requirements for Magnetic Drilling Machines
- Magnetic Materials Producers Association (MMPA) Neodymium Iron Boron Magnet Performance Characteristics
- Industrial Tool and Supply Association (ITSA) Best Practices for Magnetic Drill Press Operation and Maintenance
- Occupational Safety and Health Administration (OSHA) Powered Tool Safety Guidelines for Metal Fabrication
YS Machine Tools Co., Ltd.
We’re well-known as one of the leading magnetic drill press suppliers in China, featured by quality products and good service. Please rest assured to buy customized magnetic drill press at competitive price from our factory. Contact us for more details.
Address: 300 Sandusky st, Ohio, 43611, USA
E-mail: yishoumachinetools@gmail.com
WebSite: https://www.ysmachinetool.com/
